

07-21-2018, 11:02 PM
I don't install a barrel before doing several things:
1. I visually inspect everything about the barrel, extension, muzzle threads, and look for presence of a burr at the gas port in the bore. I look at the bore to make sure it has rifling in it and that all looks normal. (You'd think that sounds silly, but sadly, it's not.)
2. I check that all my dummy cartridges will chamber fully, and fall out with gravity or a light tap into my palm.
3. I inspect the bolt, lugs, face depth, extractor, ejector, bolt face sharpness around the ejector channel, sharpness of the extractor pocket/bolt face ledge, and deal with each of those areas if needed. I normally radius the ejector after removing it, and will ensure the ejector channel is free from burrs and machine marks. These are sometimes left over from the manufacturing process where the particular shop is focused on cranking volume, as opposed to detailed, quality inspections. As a builder, you now get to deal with this yourself.
4. I de-edge, blend, and polish the barrel extension. The only extensions I've seen where I didn't need to do this were the initial Lilja group buy barrels that used BAT Machine extensions. Those were works of art in the world of barrel extensions, perfect in about every way. The metallurgy was top-notch, concentricity, fit, and tumble polish removed any sharp edges we normally see.
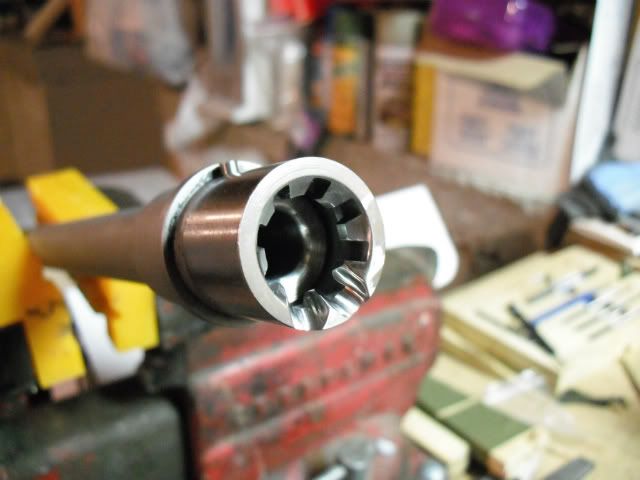
Some extensions that I've done this to have very large grain structure, and appeared to be of lesser quality steel. I don't get a warm a fuzzy feeling when I see that. Others have been so hard from the nitride process that the lips cracked off like obsidian with just a rubber Cratex polishing bit (rubber/elastomer with impregnated fine polish media).
A lot of the extensions we're seeing nowadays show no signs of finish work in terms of taking the edges off, or removing burrs. If you go to chamber the action, the bolt lugs can drag or gall the burrs, or break pieces off and slam them into your chamber or bolt lug recess area in the extension.
Part of assembling the rifle yourself now is that you are the final check station in quality control, so while the TDP M16s and M4s are plug and play by call-out and specific lines in the Mil-Std documents, civilian parts do not adhere to those technical drawings and interoperability requirements set forth in the Military specifications.
That means some hand-fitting might be required, and if you're not exactly sure of what you're doing, this can be a problem.
Since the barrel extension is a pressure containment component with specific heat treat, how much material and where do you polish it? If the barrel maker was loose on their specs and QC for heat treat on what went into your barrel, knowing that he or she wasn't going to be test-firing it anyway, taking a grinder to it could present some problems.
I've already seen several cases now where people have had barrel extensions fail on them, which is normally rare. When you become the final assembler, you assume a lot more responsibility than in a normal scenario where you simply buy a complete rifle that has been tested by the manufacturer.
1. I visually inspect everything about the barrel, extension, muzzle threads, and look for presence of a burr at the gas port in the bore. I look at the bore to make sure it has rifling in it and that all looks normal. (You'd think that sounds silly, but sadly, it's not.)
2. I check that all my dummy cartridges will chamber fully, and fall out with gravity or a light tap into my palm.
3. I inspect the bolt, lugs, face depth, extractor, ejector, bolt face sharpness around the ejector channel, sharpness of the extractor pocket/bolt face ledge, and deal with each of those areas if needed. I normally radius the ejector after removing it, and will ensure the ejector channel is free from burrs and machine marks. These are sometimes left over from the manufacturing process where the particular shop is focused on cranking volume, as opposed to detailed, quality inspections. As a builder, you now get to deal with this yourself.
4. I de-edge, blend, and polish the barrel extension. The only extensions I've seen where I didn't need to do this were the initial Lilja group buy barrels that used BAT Machine extensions. Those were works of art in the world of barrel extensions, perfect in about every way. The metallurgy was top-notch, concentricity, fit, and tumble polish removed any sharp edges we normally see.
Some extensions that I've done this to have very large grain structure, and appeared to be of lesser quality steel. I don't get a warm a fuzzy feeling when I see that. Others have been so hard from the nitride process that the lips cracked off like obsidian with just a rubber Cratex polishing bit (rubber/elastomer with impregnated fine polish media).
A lot of the extensions we're seeing nowadays show no signs of finish work in terms of taking the edges off, or removing burrs. If you go to chamber the action, the bolt lugs can drag or gall the burrs, or break pieces off and slam them into your chamber or bolt lug recess area in the extension.
Part of assembling the rifle yourself now is that you are the final check station in quality control, so while the TDP M16s and M4s are plug and play by call-out and specific lines in the Mil-Std documents, civilian parts do not adhere to those technical drawings and interoperability requirements set forth in the Military specifications.
That means some hand-fitting might be required, and if you're not exactly sure of what you're doing, this can be a problem.
Since the barrel extension is a pressure containment component with specific heat treat, how much material and where do you polish it? If the barrel maker was loose on their specs and QC for heat treat on what went into your barrel, knowing that he or she wasn't going to be test-firing it anyway, taking a grinder to it could present some problems.
I've already seen several cases now where people have had barrel extensions fail on them, which is normally rare. When you become the final assembler, you assume a lot more responsibility than in a normal scenario where you simply buy a complete rifle that has been tested by the manufacturer.
NRA Basic, Pistol, Rifle, Shotgun, RSO
CCW, CQM, DM, Long Range Rifle Instructor
6.5 Grendel Reloading Handbooks & chamber brushes can be found here:
www.AR15buildbox.com
CCW, CQM, DM, Long Range Rifle Instructor
6.5 Grendel Reloading Handbooks & chamber brushes can be found here:
www.AR15buildbox.com